Uncategorized

Uncategorized

Baggage Handling Design Consultancy: The Key to Efficient Airport Operations

Modern airports depend on efficient baggage handling systems to keep operations running smoothly. From the moment a passenger checks in luggage until it arrives at the destination carousel, every step must be carefully planned and executed. This is where professional baggage handling design consultancy becomes essential. At Mexeltec, we specialize in providing intelligent baggage handling design solutions that help airports improve efficiency, reduce operational costs, and enhance passenger experiences. What Is Baggage Handling Design Consultancy? Baggage handling design consultancy involves planning, analyzing, and optimizing the systems responsible for transporting luggage throughout an airport. Rather than simply installing conveyors and equipment, consultants evaluate: Airport capacity requirements Passenger traffic forecasts Terminal layouts Operational workflows Future expansion plans Maintenance accessibility The result is a customized baggage handling solution designed specifically for the airport’s needs. Why Airports Need Expert Design Consultancy Increasing Passenger Numbers Global air travel continues to grow, placing greater demands on airport infrastructure. Without proper planning, baggage systems can quickly become bottlenecks that slow operations and create passenger frustration. Operational Efficiency An optimized baggage handling system ensures luggage moves efficiently through check-in, screening, sorting, transportation, and reclaim areas. This improves overall airport performance while reducing delays. Cost Savings Strategic system design helps airports avoid expensive modifications and operational inefficiencies later. Investing in expert consultancy during the planning stage often leads to significant long-term savings. Key Components of a Modern Baggage Handling System Conveyor Networks Conveyors form the foundation of baggage transportation throughout the airport. Proper conveyor design ensures reliable and continuous baggage movement. Sorting Systems Advanced sorting solutions direct luggage to the correct flights with speed and accuracy. Security Screening Integration Modern baggage systems must seamlessly integrate with security screening processes while maintaining throughput efficiency. Control Systems Intelligent control systems monitor baggage movement and optimize operational performance. Benefits of Professional Baggage Handling Design Enhanced Passenger Experience Passengers expect their baggage to arrive quickly and safely. Efficient systems reduce delays and improve customer satisfaction. Improved Throughput Capacity Well-designed systems handle increasing baggage volumes without compromising performance. Reduced Maintenance Costs Smart layouts simplify maintenance access and reduce downtime. Scalability Future airport expansions become easier when scalability is incorporated into the initial design. How Mexeltec Supports Airport Projects Mexeltec provides end-to-end baggage handling consultancy services including: Concept Development We evaluate project requirements and develop efficient system concepts. Layout Design Our engineers create optimized layouts that maximize available space. Capacity Planning We analyze passenger and baggage forecasts to ensure future readiness. Technical Support Our team provides detailed technical guidance throughout the project lifecycle. Expansion Strategy We help airports prepare for future growth without requiring complete system redesigns. Trends Shaping the Future of Baggage Handling The airport industry is rapidly evolving. Key trends include: Automated baggage handling systems RFID baggage tracking Artificial intelligence-driven monitoring Energy-efficient conveyor technologies Predictive maintenance systems Airports that adopt these innovations can achieve higher efficiency and better passenger satisfaction. Choosing the Right Baggage Handling Design Consultancy When selecting a consultancy partner, consider: Industry experience Technical expertise Project portfolio Scalability capabilities Long-term support services A knowledgeable consultancy partner can significantly improve project outcomes and return on investment. Conclusion Efficient baggage handling systems are essential for modern airport operations. From passenger satisfaction to operational performance, every aspect of airport success depends on reliable baggage movement. Mexeltec provides professional baggage handling design consultancy services that help airports create smarter, more efficient, and future-ready systems. Whether you’re planning a new airport facility or upgrading an existing one, our team can help deliver solutions tailored to your operational goals. Contact Mexeltec today to discuss your baggage handling project requirements. Website: www.mexeltec.com Email: info@mexeltec.com

Baggage Handling Design Consultancy: The Key to Efficient Airport Operations Read Post »
Uncategorized

How to Choose the Right Airport Counter Supplier for Your Project

When planning an airport terminal project, most stakeholders focus on major infrastructure components such as baggage handling systems, security equipment, and passenger boarding bridges. However, one critical element that directly affects passenger experience and operational efficiency is often overlooked: airport counters. From check-in counters and information desks to boarding gate counters and customer service stations, these installations play a crucial role in daily airport operations. Choosing the right airport counter supplier can determine whether your project runs smoothly or faces costly delays, maintenance issues, and operational inefficiencies. At Mexeltec, we work with airports, consultants, contractors, and aviation infrastructure developers to deliver custom airport counter solutions that meet modern industry requirements. Based on our experience, here’s a comprehensive guide to selecting the right supplier for your airport project. Why Selecting the Right Airport Counter Supplier Matters Airport counters are not ordinary furniture. They must withstand thousands of passenger interactions daily while supporting airport staff, technology systems, security requirements, and operational workflows. The wrong supplier can result in: Delayed project completion Poor-quality materials High maintenance costs Operational disruptions Passenger dissatisfaction Expensive future modifications The right supplier helps ensure long-term performance, reliability, and value for your investment. Understand Your Project Requirements First Before contacting suppliers, clearly define your project requirements. Ask yourself: Is this a new airport project or terminal expansion? How many counters are required? What functions will they serve? What technologies need integration? What are the expected passenger volumes? What are the project timelines? Having clear specifications helps suppliers provide accurate proposals and recommendations. Look for Industry Experience Experience matters in airport infrastructure projects. Airport environments are very different from commercial offices or retail spaces. An experienced supplier understands: Airport operational requirements Passenger flow considerations Aviation industry standards Security regulations Technology integration needs High-traffic durability requirements Always ask suppliers about their airport project experience and previous installations. Evaluate Design Capabilities Every airport has unique operational needs. Avoid suppliers that only offer standard designs. Instead, choose a supplier capable of providing: Custom designs Layout optimization Space planning Ergonomic solutions Future-ready configurations The ability to customize airport counters ensures better alignment with terminal operations and passenger expectations. Assess Manufacturing Quality Airport counters operate continuously under demanding conditions. Quality should never be compromised. Look for suppliers that use: Premium-grade materials Durable structural frameworks Commercial-grade finishes High-quality hardware Corrosion-resistant components Ask about manufacturing processes, quality control procedures, and testing methods. A well-built counter may last significantly longer and reduce lifecycle costs. Check Technology Integration Capabilities Modern airport counters must support various technologies. These may include: Computer systems Boarding equipment Passport scanners Self-service technologies Digital displays Network infrastructure Power and data connections The supplier should be able to design counters that accommodate current and future technology requirements. Consider Passenger Experience Passenger expectations continue to evolve. Today’s travelers expect: Fast service Comfortable interactions Accessible facilities Modern aesthetics The right supplier understands how design impacts customer satisfaction and can recommend solutions that enhance the passenger journey. Verify Accessibility Compliance Accessibility is no longer optional. Airport counters should comply with applicable accessibility standards and regulations. Features may include: Accessible service positions Appropriate counter heights Wheelchair access Clear visibility Inclusive layouts A knowledgeable supplier will incorporate accessibility requirements during the design phase. Review Material Options Carefully Different materials offer different advantages. Common options include: Solid Surface Materials Benefits: Premium appearance Easy maintenance Long lifespan Stainless Steel Components Benefits: Durability Corrosion resistance Professional appearance High-Pressure Laminates Benefits: Cost-effective Wide design options Easy cleaning The right supplier will help select materials based on budget, aesthetics, and operational requirements. Ask About Installation Services Many airport projects fail because of poor installation planning. Choose a supplier that offers: Installation support Site supervision Coordination with contractors Project management assistance Professional installation minimizes disruptions and ensures proper functionality. Evaluate Maintenance Requirements Maintenance costs continue long after installation. Ask suppliers: How easy is maintenance? Are spare parts available? What is the expected lifespan? How quickly can repairs be completed? Counters designed for easy maintenance reduce operational downtime. Review Previous Projects One of the best ways to evaluate a supplier is by reviewing previous work. Request: Project portfolios Case studies Reference projects Client testimonials Look for projects similar to your own airport requirements. Successful project history often indicates future reliability. Assess Project Management Capabilities Airport projects involve multiple stakeholders. A reliable supplier should have strong project management processes covering: Design reviews Manufacturing schedules Logistics coordination Installation planning Final commissioning Good project management reduces risks and improves delivery performance. Don’t Base Decisions Solely on Price Many buyers make the mistake of selecting the lowest quotation. The cheapest option often becomes the most expensive over time. Instead, evaluate: Product quality Supplier expertise Support services Installation capabilities Long-term maintenance costs Project delivery reliability Focus on total value rather than initial cost alone. Questions to Ask Every Airport Counter Supplier Before making a final decision, ask: How many airport projects have you completed? Can you provide airport-specific references? Do you offer custom counter designs? What materials do you use? Can your counters integrate airport technologies? What quality control measures do you follow? Do you provide installation support? What warranties do you offer? What is your project delivery timeline? How do you handle after-sales support? The answers will quickly reveal which suppliers are best suited for your project. Why Airports Choose Mexeltec At Mexeltec, we provide complete airport counter solutions tailored to the unique requirements of modern airports. Our services include: Airport counter design Manufacturing Supply Installation Testing Commissioning We focus on delivering solutions that combine durability, functionality, passenger comfort, and operational efficiency. Whether you’re constructing a new terminal, expanding an airport, or upgrading existing facilities, our team works closely with consultants, contractors, and airport authorities to achieve successful project outcomes. Final Thoughts Choosing the right airport counter supplier is a strategic decision that impacts airport operations for years to come. The ideal supplier should offer more than just products. They should provide expertise, quality, customization, project management, and long-term support. By carefully evaluating experience, manufacturing quality, technology integration, and service capabilities,

How to Choose the Right Airport Counter Supplier for Your Project Read Post »

Uncategorized

Airport Baggage Handling Design Trends Every Aviation Consultant Should Know

  The aviation industry is evolving faster than ever. Passenger expectations are increasing, airport infrastructure is expanding, and operational efficiency has become a top priority for airports worldwide. In 2026, baggage handling systems are no longer viewed as simple conveyor networks — they are now considered mission-critical airport infrastructure. For aviation consultants, staying updated with the latest baggage handling design trends is essential for delivering future-ready airport solutions. At Mexeltec, we specialize in advanced baggage handling design consultancy, helping airports create scalable, intelligent, and high-performance systems tailored to modern aviation demands. If you are involved in airport planning, aviation infrastructure, or baggage handling consultancy, these are the key trends shaping the future of airport baggage handling systems. 1. Smart Automation Is Becoming the Standard Traditional baggage handling systems relied heavily on manual intervention. That model is rapidly disappearing. Modern airports are investing in intelligent automation to improve speed, accuracy, and operational efficiency. Automated baggage handling systems reduce human error, increase throughput, and improve passenger satisfaction. Today’s smart baggage systems include: Automated sortation systems Intelligent conveyor routing Real-time baggage tracking Automated scanning and screening Smart load balancing AI-driven operational monitoring Airports that fail to modernize their baggage infrastructure risk delays, congestion, and poor passenger experiences. For aviation consultants, automation planning is no longer optional — it is a necessity. 2. Scalability Is Now a Core Design Requirement One of the biggest mistakes airports make is designing baggage systems only for current passenger traffic. The reality is simple: Passenger volumes will continue to grow. Modern baggage handling design must support future expansion without requiring complete system replacement. That means consultants must focus on: Modular conveyor layouts Expandable sortation systems Flexible routing strategies Space-efficient system architecture Future terminal integration planning At Mexeltec, scalability is a key part of every baggage handling consultancy project because airports need infrastructure that grows with operational demand. 3. Passenger Experience Is Driving System Design Airports are becoming highly customer-focused environments. Passengers expect: Faster baggage delivery Minimal waiting time Real-time baggage visibility Fewer lost luggage incidents Smooth airport movement This shift is changing how baggage handling systems are designed. Modern consultants must optimize systems for both operational efficiency and passenger satisfaction. Design priorities now include: Faster reclaim systems Reduced transfer times Intelligent baggage routing Real-time baggage information systems Congestion-free layouts The airports delivering the best passenger experiences are investing heavily in baggage handling modernization. 4. Data-Driven Operations Are Transforming Airports Airport operators now rely on operational data to improve performance and decision-making. This is why modern baggage handling systems are increasingly integrated with: IoT sensors Predictive analytics AI-based monitoring Digital twins Centralized control systems Performance dashboards These technologies help airports: Predict maintenance issues Reduce downtime Optimize conveyor performance Improve baggage tracking accuracy Increase operational visibility For aviation consultants, understanding smart airport technologies is becoming just as important as understanding conveyor mechanics. 5. Inline Security Screening Integration Is Expanding Security requirements continue to evolve globally. Modern airports now integrate baggage screening directly into baggage handling systems rather than treating security as a separate process. This trend improves: Passenger flow Operational efficiency Security compliance Space utilization Modern baggage handling consultancy now requires expertise in: Inline screening integration Security checkpoint optimization Explosive detection system coordination Conveyor screening interfaces Compliance planning Aviation consultants must ensure security integration happens seamlessly without slowing airport operations. 6. Sustainability Is Influencing Airport Infrastructure Decisions Sustainability is no longer a marketing buzzword. Airports worldwide are under pressure to reduce energy consumption and improve environmental performance. This directly impacts baggage handling system design. Modern airports are looking for: Energy-efficient conveyor motors Smart power management Reduced system downtime Sustainable material selection Lower operational waste Efficient layout planning Consultants who understand sustainable baggage handling design will have a significant competitive advantage in the coming years. 7. Supplier-Neutral Consultancy Is Becoming More Valuable Airports are increasingly seeking independent, supplier-neutral baggage handling consultants. Why? Because airports want solutions optimized for operational performance — not systems designed around a single manufacturer’s products. Supplier-neutral consultancy provides: Objective system recommendations Better long-term flexibility Competitive procurement opportunities Optimized operational planning Technology adaptability At Mexeltec, we focus on performance-driven baggage handling consultancy tailored to each airport’s operational goals and infrastructure requirements. 8. Digital Simulation and System Modeling Are Now Essential Before modern airports invest millions into baggage handling infrastructure, they want proof that systems will perform efficiently. This is why digital simulation has become a major trend. Consultants now use advanced modeling tools to simulate: Passenger traffic flow Conveyor throughput Peak operational loads Transfer baggage movement Bottleneck analysis System redundancy performance Simulation-based consultancy helps airports reduce risk and improve decision-making before implementation begins. 9. High-Speed Sortation Systems Are Growing in Demand As airports become busier, baggage handling speed becomes critical. Modern airports require high-speed sortation systems capable of handling large baggage volumes without compromising accuracy. This trend is driving demand for: Tilt-tray sorters Cross-belt sorters High-speed diverters Smart routing systems Dynamic conveyor controls For consultants, understanding advanced sortation technologies is becoming increasingly important for large airport projects. 10. Integrated Airport Infrastructure Planning Is the Future Baggage handling systems no longer operate independently. Modern airport design focuses on complete infrastructure integration involving: Passenger flow systems Security operations Check-in systems Aircraft turnaround operations Terminal management systems Logistics coordination This integrated approach improves overall airport efficiency and operational performance. The future belongs to consultants who understand how baggage handling fits into the bigger airport ecosystem. Final Thoughts Airport baggage handling systems are evolving rapidly, and aviation consultants must adapt to changing technologies, operational demands, and passenger expectations. From automation and AI integration to sustainability and smart infrastructure planning, the future of baggage handling consultancy is centered around intelligent, scalable, and performance-driven system design. Airports that invest in modern baggage handling infrastructure today will gain a significant operational advantage tomorrow. At Mexeltec, we provide expert baggage handling design consultancy solutions focused on innovation, efficiency, scalability, and long-term airport performance. Our consultancy services help airports build smarter baggage handling systems that meet the demands of modern aviation infrastructure.

Airport Baggage Handling Design Trends Every Aviation Consultant Should Know Read Post »

Uncategorized

Belt Conveyor vs Roller Conveyor: Which Is Best for Your Industry?

When businesses invest in material handling systems, one decision can directly impact productivity, operational costs, and long-term efficiency: Should you choose a belt conveyor or a roller conveyor? This isn’t just about moving products from point A to point B. It’s about choosing the right system that boosts workflow, reduces downtime, and scales with your business. The wrong choice can slow operations, increase maintenance costs, and create unnecessary bottlenecks. The right choice? It can transform your warehouse, airport, logistics hub, or manufacturing plant. In this guide, you’ll discover: The key differences between belt conveyors and roller conveyors The pros and cons of each system Which industries benefit most from each How to choose the best conveyor for your business Let’s dive in. What Is a Belt Conveyor? A belt conveyor uses a continuous moving belt powered by motors to transport products smoothly across distances. It’s ideal for: Warehouses Airports Food processing Packaging industries Manufacturing plants Key Benefits of Belt Conveyors: 1. Handles a Wide Variety of Products From cartons to loose materials, belt conveyors are highly versatile. 2. Smooth Transportation Products remain stable during movement, reducing product damage. 3. Ideal for Inclines and Declines Need to move products upward or downward? Belt conveyors excel here. 4. Automation-Friendly Perfect for modern warehouses integrating smart automation. Potential Downsides: Higher initial cost Belt replacement over time More maintenance than gravity roller systems What Is a Roller Conveyor? A roller conveyor uses cylindrical rollers to move goods manually, by gravity, or motorized systems. It’s commonly used in: Distribution centers Assembly lines Courier sorting Manufacturing Packaging zones Key Benefits of Roller Conveyors: 1. Cost-Effective Especially for transporting uniform boxes and pallets. 2. Low Maintenance Fewer moving parts often mean reduced maintenance. 3. Modular and Flexible Can be expanded or customized easily. 4. Excellent for Heavy Loads Great for cartons, pallets, and industrial products. Potential Downsides: Less effective for irregular or fragile products Not ideal for steep inclines May require specific product dimensions Belt Conveyor vs Roller Conveyor: Side-by-Side Comparison 1. Product Type Belt Conveyor: Best for fragile, irregular, or mixed-size productsRoller Conveyor: Best for boxes, pallets, and consistent loads 2. Cost Belt Conveyor: Higher upfront investmentRoller Conveyor: More budget-friendly 3. Maintenance Belt Conveyor: ModerateRoller Conveyor: Low to moderate 4. Speed & Automation Belt Conveyor: Better for automated, high-speed systemsRoller Conveyor: Excellent for controlled transport 5. Industry Applications Belt Conveyor: Airports, food, pharmaceuticals, warehousingRoller Conveyor: Logistics, manufacturing, e-commerce sorting Which Industries Should Choose Belt Conveyors? Choose Belt Conveyors If You: Handle delicate or irregular items Need incline or decline movement Operate airport baggage systems Require continuous automated transport Need cleaner product movement Best For: Airports Warehouses FMCG Pharmaceuticals Food industries Which Industries Should Choose Roller Conveyors? Choose Roller Conveyors If You: Handle boxes, cartons, or pallets Want lower investment Need modular systems Focus on heavy-duty transport Operate assembly or packaging lines Best For: Logistics Courier hubs E-commerce Manufacturing Packaging The Hidden Cost Most Businesses Ignore Many businesses choose based only on price. That’s a mistake. A cheaper conveyor that reduces productivity or increases downtime can cost far more in the long run. Instead, evaluate: Product type Throughput volume Maintenance cost Future scalability Automation needs Why Custom Conveyor Solutions Matter No two industries are identical. That’s why leading suppliers like Mexeltec design customized conveyor solutions for: Airports Warehouses Logistics hubs Manufacturing facilities Custom systems improve: Efficiency Safety Scalability ROI Final Verdict: Belt Conveyor or Roller Conveyor? Choose Belt Conveyor for: Versatility + Automation + Fragile Product Handling Choose Roller Conveyor for: Cost Savings + Heavy Loads + Simplicity Bottom Line Your conveyor system is not an expense. It’s a growth investment. The right system can: Increase operational speed Reduce labor costs Improve customer satisfaction Scale your business If you’re planning a conveyor upgrade, focus on long-term business goals—not just initial cost. Need Expert Conveyor Guidance? Mexeltec provides custom-engineered belt and roller conveyor solutions for warehouses, airports, logistics, and industrial operations. Get in touch today:Email: info@mexeltec.comWebsite: www.mexeltec.com

Belt Conveyor vs Roller Conveyor: Which Is Best for Your Industry? Read Post »

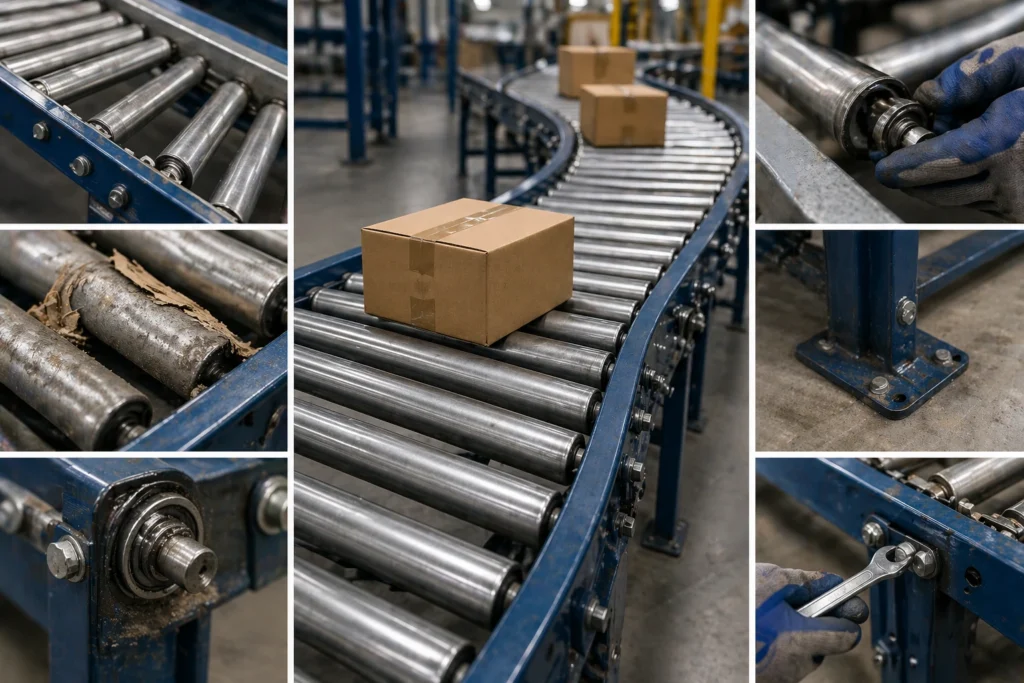
Industrial roller conveyor system showing common maintenance issues such as dirty rollers, misalignment, worn bearings, and repair work in a warehouse setting.
Uncategorized

Common Problems in Roller Conveyors and How to Fix Them (Complete Guide)

Roller conveyors are the backbone of modern material handling systems. From warehouses to airports, they keep operations moving efficiently. But here’s the reality:Even the best conveyor systems face problems. The difference between smooth operations and costly downtime????? Knowing what to fix—and when. In this guide, we’ll break down the most common roller conveyor problems and exactly how to solve them.  1. Rollers Not Moving Smoothly The Problem: You notice jerky movement or resistance in the rollers. Causes: Solution: ✔ Clean rollers regularly✔ Replace damaged bearings✔ Check alignment across the frame The Problem: Products drift to one side, causing jams. Causes: Solution: ✔ Realign rollers properly✔ Ensure level installation✔ Use precision-engineered systems The Problem: Loud, unusual noises during operation. Causes: Solution: ✔ Lubricate moving parts✔ Tighten bolts and fasteners✔ Upgrade to high-quality rollers The Problem: Goods get stuck, slowing down operations. Causes: Solution: ✔ Optimize roller diameter & pitch✔ Avoid exceeding load limits✔ Customize system for your application The Problem: The system suddenly stops working. Causes: Solution: ✔ Perform regular motor checks✔ Install overload protection✔ Schedule preventive maintenance The Problem: Rollers wear out faster than expected. Causes: Solution: ✔ Invest in high-quality systems✔ Follow load capacity guidelines✔ Implement maintenance schedules Here’s what most businesses overlook: ???? Problems don’t start during operation—they start during design. A poorly designed conveyor system will always fail faster. This is where most companies lose money. Instead of buying a “standard conveyor,” you need a custom-engineered solution. At Mexeltec, you get: ✔ Precision-designed roller conveyors✔ High-quality materials for long life✔ Solutions for airports, warehouses & industries✔ Complete support from design to installation Roller conveyor issues are common—but they’re also preventable. If you: ???? You eliminate downtime and maximize ROI. If you’re facing issues or planning a new installation, Mexeltec can help you design a reliable, high-performance solution. ???? Contact us today for a custom consultation.

Common Problems in Roller Conveyors and How to Fix Them (Complete Guide) Read Post »

Uncategorized

Common Mistakes to Avoid When Installing a Custom Roller Conveyor

Installing a custom roller conveyor should boost efficiency, not add problems. But here’s the reality:Most conveyor issues don’t come from the equipment.They come from mistakes made before and during installation. The good news?You can avoid all of them — and Mexeltec can help you do it right the first time. Let’s break down the biggest installation mistakes and how to avoid them. 1. Not Defining the Real Purpose of the Conveyor Most conveyor failures start with unclear goals. If you don’t know exactly what the conveyor should do—Move heavy loads? Speed up order picking? Improve baggage handling? Automate truck loading?—your system will never be optimized. Fix: Define the purpose clearly. Mexeltec designs custom roller conveyors based on your exact operational needs so you don’t waste money on the wrong setup. 2. Ignoring Load Specifications Rollers don’t break because they’re weak.They break because the wrong roller type was selected. Every roller has limits: Load per roller Conveying speed Material suitability Guessing these specs = guaranteed downtime. Fix: Know your load requirements before selecting rollers. Mexeltec calculates load capacity and speed needs to ensure long-term performance. 3. Poor Layout Planning A poor conveyor layout slows everything down.Worse—fixing it later is expensive and disruptive. Bottlenecks, unnecessary turns, and bad flow design can ruin your throughput. Fix: Map material flow first. At Mexeltec, we plan layouts that eliminate workflow friction and maximize floor space. 4. Forgetting Future Expansion A conveyor built only for today becomes a bottleneck tomorrow. If your business grows, your conveyor must scale with it. Fix: Choose modular designs. Mexeltec builds expandable conveyor systems so you can scale without full replacements. 5. Underestimating Safety Requirements Skipping safety during installation is a major risk. Missing emergency stops, roller guards, or safety rails can cost you far more later. Fix: Follow safety standards. Mexeltec integrates international safety compliance into every installation. 6. Installing Without Proper Leveling A slightly uneven roller conveyor creates huge problems: Load drifting Roller jamming Excess noise Motor stress Precision matters. Fix: Level the conveyor perfectly. Mexeltec uses professional alignment tools to ensure flawless installation. 7. Skipping Testing & Calibration “Install → Turn on → Hope for the best”This is the most common mistake. A conveyor needs proper testing, including: Load simulation Alignment check Speed calibration Full dry runs Skipping these steps invites operational failures. Fix: Test everything before going live. Mexeltec performs full commissioning and testing on every installation. Final Thoughts A custom roller conveyor is an investment.Avoiding these mistakes ensures it delivers maximum efficiency, safety, and ROI. If you want expert installation, planning, and long-term support, Mexeltec provides complete conveyor solutions — from design to commissioning.

Common Mistakes to Avoid When Installing a Custom Roller Conveyor Read Post »

Uncategorized

How Material Handling Solutions Improve Efficiency in Airports & Logistics Hubs

How Material Handling Solutions Improve Efficiency in Airports & Logistics Hubs If you look closely at the busiest airports or logistics hubs in the world, you will notice something interesting. The ground looks calm. Bags move. Parcels flow. Conveyors hum. Passengers glide through. Trucks load faster. Warehouses stay organised. Every system looks predictable and controlled. But behind this “effortless” movement lies a powerful ecosystem: material handling solutions—the backbone of every operationally strong airport and logistics hub. Most people think material handling solutions are just conveyors, tubs, or counters. But in reality? They are productivity multipliers. They are time savers. And they are profit boosters. In this guide, you’ll discover exactly how material handling solutions improve efficiency in airports and logistics hubs, why the biggest global brands invest heavily in them, and what you should prioritise when choosing the right partner.   1. The Real Meaning of Material Handling Solutions (and Why It Matters) Before we jump into efficiency gains, let’s get one thing straight. Material handling solutions are not individual machines—they are systems. A system designed to: Move materials safely Reduce operational waste Improve speed Increase accuracy Make processes predictable Reduce manual labour Eliminate bottlenecks Increase throughput Think about any airport. Nothing there is random. Every movement—bags, cargo, trays, trolleys, and people—is controlled by a carefully engineered material handling system. At logistics hubs and warehouses, the same story repeats. Whether it’s: Shipping parcels Sorting goods Unloading trucks Loading pallets Moving products to storage Dispatching orders …everything relies on the strength of the underlying material handling solutions.   2. Why Airports Can’t Function Without Material Handling Solutions Airports operate under tremendous pressure. Every minute counts. Every delay costs money. Every mistake causes operational chaos. Without strong material handling systems, airports face: Passenger dissatisfaction Lost baggage incidents Congested checkpoints Slow baggage delivery Security risks Delayed aircraft turnaround This is why airports invest in multiple components of the material-handling ecosystem, such as: ✔ Belt Conveyors For fast and smooth baggage movement. ✔ Roller Conveyors For manual inspection zones and load transfers. ✔ Baggage Tubs To protect passenger luggage during scanning and handling. ✔ Airport Check-In Counters To create organised, fast-moving passenger flow. ✔ Security Screening Systems X-rays, metal detectors, and tray return systems. ✔ Sorting Systems To ensure each bag reaches the right aircraft. Together, these become the invisible “blood vessels” of every busy airport. 3. How Material Handling Solutions Make Logistics Hubs More Efficient Logistics hubs have one primary objective: Move goods faster with fewer errors. Unlike airports, logistics hubs deal with total volume and speed of delivery. If they fail at this, everything collapses: Delayed shipments Customer complaints Returns and refunds Low warehouse productivity Increased labour cost Breakdowns in the supply chain Material handling solutions solve all these problems with: ✔ Automated Conveyor Systems For seamless, uninterrupted parcel movement. ✔ Sorting Conveyors To streamline distribution by size, weight, or destination. ✔ Loading & Unloading Conveyors Especially truck loading conveyors—the highest ROI system in logistics. ✔ Pallet Handling Systems To automate warehouse storage and retrieval. ✔ Carton Flow Systems To speed up picking and replenishment. The result? Faster order fulfilment. Better accuracy. Lower cost per shipment. Reduced manual handling. Higher throughput. 4. The ROI of Investing in Material Handling Solutions Businesses don’t invest in material handling systems just because they “look modern.” They do it because the returns are massive. Here’s how material handling solutions deliver ROI: 1. Speed — Faster Operations Conveyors don’t take breaks. They don’t get tired. They run 24/7 and move items faster than humans. 2. Cost Savings — Reduced Manual Labour Less manpower = fewer injuries + lower salaries + fewer errors. 3. Accuracy — Zero Guesswork Automation removes the randomness of human decisions. 4. Space Efficiency Better systems → more use of vertical and horizontal space. 5. Reduced Damage Material moves smoothly, safely, and consistently. 6. Better Throughput When everything flows like clockwork, total output increases. This is why top airports and logistics hubs across the world adopt strong material handling solutions early—they understand the compounding effect. 5. The Most Important Material Handling Systems for Airports Let’s break this down into airport-specific components: ✔ Airport Conveyors (Belt & Roller) These move: Check-in baggage Security trays Transit luggage Oversized items Strong conveyors reduce waiting time and improve aircraft turnaround. ✔ Baggage Tubs These protect fragile and small items inside x-ray machines and transport belts. ✔ Airport Check-In Counters A professionally designed counter can handle: High passenger volumes Faster transactions Smoother queue management ✔ Baggage Handling Systems This includes: Sorting Tagging Loading Unloading Transfer operations ✔ Security Checkpoint Conveyors For trays and passenger belongings. Together, these systems determine the overall airport experience. 6. The Most Important Material Handling Systems for Logistics Hubs Now let’s talk logistics hubs—these rely heavily on engineered systems that increase total volume. ✔ Truck Loading Conveyors These reduce loading/unloading time by more than 50%. ✔ Sorting Conveyors For rapid parcel classification. ✔ Powered & Gravity Roller Conveyors Ideal for manual zones. ✔ Belt Conveyors For long-distance transport within facilities. ✔ Pallet Conveying & Racking Systems Helps with systematic storage. ✔ Scanning & Labelling Integration Makes order processing predictable. These systems transform manual warehouses into high-performance distribution machines. 7. 10 Ways Material Handling Solutions Improve Efficiency To summarise the real performance gains: Faster baggage or parcel movement Reduced human error Higher throughput Shorter turnaround time Better safety Controlled traffic flow Reduced labour dependency Minimal product damage Higher storage utilisation Predictable daily operations 8. Why Choosing the Right Material Handling Partner Matters You can buy machines from anywhere. But material handling solutions? You need expertise, engineering knowledge, and installation accuracy. A wrong calculation = breakdown costs A wrong alignment = unsafe movement A wrong design = low throughput Wrong installation = continuous maintenance issues This is where Mexeltec stands out. 9. Why Mexeltec? Mexeltec offers complete material handling solutions for: Industries Airports Warehouses Logistics centres Including: Roller conveyors Belt conveyors Airport counters Baggage tubs Baggage handling systems Airport conveyor installation End-to-end design, supply & commissioning

How Material Handling Solutions Improve Efficiency in Airports & Logistics Hubs Read Post »

Uncategorized

How Automated Truck Loading Systems Reduce Labour Costs and Safety Risks

How Automated Truck Loading Systems Reduce Labour Costs and Safety Risks If you’re still loading trucks manually in 2025, I’m going to be blunt: You’re wasting money. You’re slowing down your operations. And you’re exposing your team to unnecessary risks. The truth? Manual truck loading feels “normal” because warehouses have done it the same way for decades. But normal doesn’t mean efficient. And it definitely doesn’t mean profitable. Today, the smartest logistics companies are switching to Automated Truck Loading Systems (ATLS) — and seeing massive improvements within weeks. Let’s break it down in a simple, ROI-focused way. The Hidden Costs Nobody Calculates (But Every Warehouse Pays) Most warehouse managers think manual loading is cheap because you’re paying people instead of buying automation. But here’s the math they miss: 6–10 workers per truck 45–90 minutes of loading time High overtime expenses Frequent injuries Slower dispatch cycles Customer delays Fatigue → mistakes → product damage Add it all up and manual loading becomes one of your most expensive operations. Now the question is: Is this sustainable when labour prices keep rising and customer expectations keep tightening? (No.) What Automated Truck Loading Systems Actually Do Automated truck loading systems remove the manual effort from loading. This can include: Telescopic belt conveyors Mobile/loading conveyors Extendable boom conveyors Roller conveyors Pallet-loading automation systems Instead of people walking in and out of the truck carrying loads, the conveyor system does the heavy movement. This one shift changes EVERYTHING. 1. Labour Costs Drop Faster Than You Think Here’s where automation blows manual loading out of the water. Manpower goes from 10 to 2–3 people. Yes, really. You can reduce labour usage by 40–60% instantly. Loading time becomes predictable and faster. Manual loading: 45–90 minutes Automated loading: 10–25 minutes Imagine what that does to your daily dispatch capacity. No more seasonal hiring headaches. Automation doesn’t need training, holidays, or breaks. You finally stop managing chaos.  2. Safety Risks Drop to Near-Zero If you look at accident reports inside warehouses, one thing stands out: Truck loading is one of the most injury-prone tasks. Why? Heavy lifting Repetitive strain Slipping inside trucks Tight spaces Forklifts entering trailers Fatigue from continuous handling Automated systems remove 80–90% of these risks. And here’s something most people overlook: Fewer injuries = lower insurance premiums + reduced downtime + higher morale. That’s REAL savings.  3. Loading Speeds Increase → Customers Stay Happier Today’s supply chain moves fast. And customers expect speed — ALWAYS. When you automate: Trucks leave faster Dispatch times become more accurate Bottlenecks disappear Logistics teams stop firefighting Your delivery reliability improves This alone can turn a struggling warehouse into a high-performance operation. 4. Product Damage Drops Sharply Manual loading = human fatigue = mistakes. Boxes get dropped. Pallets get pushed incorrectly. Edges get crushed. Automated systems provide: Controlled movement Smooth transitions Consistent placement Your return rates drop. Your product losses shrink. Your customers get pristine shipments. 5. You Become Future-Ready (Your Competitors Won’t See It Coming) Automation isn’t a trend. It’s not “nice to have.” It’s the new baseline for efficient warehouses. When you automate your truck loading, you gain: Higher throughput Scalability without extra labour Ability to handle peak demand without panic Integration options with sorting, scanning, and packing automation Long-term operational stability This is what prepares your business for the next 5–10 years. Who Benefits the Most From Truck Loading Automation? If your business does frequent dispatches, ATLS can transform your operations. Especially for: Logistics & warehousing companies E-commerce fulfilment hubs Retail distribution centers Manufacturing plants Airports and cargo terminals FMCG and food & beverage companies If you load trucks daily, you should automate. No exceptions. Real-World Impact (This Is Why Companies Are Switching) Here’s what companies report after installing ATLS: ✔ 40–60% reduction in labour cost ✔ 2–4× faster truck loading ✔ 70–90% fewer workplace injuries ✔ Lower insurance premiums ✔ Higher employee satisfaction ✔ Increased truck turnaround rate ✔ More daily shipments without hiring staff This isn’t theory. This is happening right now in leading warehouses.  Final Takeaway (Read This Twice) Automated Truck Loading Systems don’t just reduce labour costs. They don’t just improve safety. They give you control over your operations. You load faster. You spend less. You protect your workers. You improve customer satisfaction. And you scale without stress. If you’re serious about efficiency and long-term profitability… ATLS is not an upgrade. It’s a necessity.

How Automated Truck Loading Systems Reduce Labour Costs and Safety Risks Read Post »

Uncategorized

10 Questions to Ask Before Buying a Roller Conveyor: A Guide by Mexeltec

If you’re running a warehouse, airport, or logistics facility, you already know that efficiency is everything. And nothing impacts it more than your roller conveyor system. Buy the wrong one, and you’re looking at delays, higher labor costs, and even safety risks. Buy the right one, and your workflow becomes smooth, reliable, and cost-efficient. At Mexeltec, we’ve been helping businesses design, supply, and install custom roller conveyor systems for years. Here’s our practical guide—10 questions you need to ask before buying a roller conveyor. Ask these, and you’ll save money, time, and headaches. Need expert advice? Contact Mexeltec for a free consultation today. 1. What Type of Roller Conveyor Do I Really Need? Roller conveyors come in gravity, powered, flexible, and modular designs. Your choice directly affects your workflow. Gravity conveyors: simple, cost-effective, manual push.   Powered conveyors: motorized, continuous movement—perfect for heavy or high-volume loads.   Pro Tip: Don’t guess. Mexeltec customizes conveyors to match exactly how your facility moves. 2. What’s My Load Capacity Requirement? Every roller conveyor has a max load per roller. Exceed it, and you risk breakdowns, downtime, and safety hazards. Know your average load and max load.   Consider size and shape of items.   Mexeltec offers heavy-duty solutions built to handle your loads safely and efficiently. 3. Do I Have Enough Space? Measure your floor space, ceiling height, and workflow paths. Poor planning = bottlenecks and wasted space.   Include room for maintenance access and future expansion.   Mexeltec provides on-site surveys and layout planning so your conveyor fits perfectly. 4. Manual or Automated? Automation can skyrocket efficiency, but not every facility needs it. Manual/gravity conveyors: fine for small loads or short distances.   Motorized systems: ideal for high-volume, repetitive operations.   Mexeltec delivers semi-automatic and fully automated solutions tailored to your workflow. 5. What Materials Will the Conveyor Handle? Different items require different rollers: Heavy boxes, pallets, baggage tubs → sturdy rollers   Fragile/lightweight items → soft or coated rollers   Mexeltec customizes rollers and surfaces to protect your goods and equipment. 6. How Easy Is Maintenance? Maintenance determines lifespan and performance. Ask about: Noise levels   Roller alignment and wear resistance   Accessibility for cleaning and repairs   Mexeltec not only installs durable systems but provides ongoing maintenance support. 7. Does the Conveyor Meet Safety Standards? Safety is non-negotiable. Check that your system: Meets OSHA or local industrial standards   Includes emergency stops, guards, and anti-slip rollers   Mexeltec designs systems with safety as a priority, protecting employees and your investment. 8. What’s the Total Cost of Ownership (TCO)? Don’t just look at the purchase price. Include: Installation costs   Energy consumption   Maintenance & repair   Downtime losses   Mexeltec helps you calculate TCO and optimize for long-term ROI. 9. Can It Integrate With Existing Systems? Your new conveyor should work seamlessly with: Automated warehouses   Baggage handling systems   Sorting & packing lines   Mexeltec builds integrated solutions for smooth, efficient workflows. 10. Who Provides After-Sales Support? A conveyor is only as good as the support behind it. Check: Warranty coverage   Spare parts availability   Local service & repair support   Mexeltec offers comprehensive after-sales support to keep your system running 24/7. The Bottom Line Most companies buy roller conveyors without asking the right questions—and pay the price later. Partner with Mexeltec, and you get a custom, safe, efficient, and reliable conveyor system designed for your workflow. Ready to get it right the first time? Schedule your free consultation with Mexeltec today.

10 Questions to Ask Before Buying a Roller Conveyor: A Guide by Mexeltec Read Post »

Uncategorized

How the Right Baggage Tubs Can Transform Airport Efficiency (and Why Mexeltec Leads the Way)

Let’s be honest: when you think of airport innovation, you probably picture advanced scanners, AI-powered security, or automated check-in counters — not baggage tubs. But here’s the thing: the humble airport baggage tub is one of the most overlooked tools for improving passenger flow, reducing damage, and boosting operational efficiency. And if you manage an airport, a ground-handling team, or a security system, understanding how the right tubs make a difference can be a game changer for your bottom line. In this guide, we’ll break down: Why baggage tubs matter more than you think How design impacts security and efficiency What makes Mexeltec’s tubs stand out in the global aviation market And how investing in durable tubs pays for itself (fast) Let’s dive in. 1. Why Baggage Tubs Matter More Than You Think Airports handle millions of items every single day. From laptops to baby strollers, every item needs to pass through a smooth, secure, and damage-free process. A single bottleneck at security can delay flights, frustrate passengers, and increase operational costs. Now, here’s the catch: baggage tubs are at the center of that process. According to airport logistics experts, even minor design improvements — like better stacking or smoother surfaces — can cut handling time by up to 15–20%. That’s a massive gain at scale. So, if you want faster security lines and fewer equipment replacements, it’s time to look at your baggage tubs. 2. Design: The Unsung Hero of Efficiency Not all tubs are created equal. Mexeltec understands that airports don’t just need containers; they need precision-engineered tools that can handle real-world challenges. Here’s what sets Mexeltec’s baggage tubs apart: HDPE (High-Density Polyethylene) Construction: Strong, lightweight, and built to withstand constant handling. HDPE is resistant to cracks and chemical wear — perfect for heavy use. X-Ray Compatible: Mexeltec’s tubs are designed for seamless integration with X-ray systems, ensuring accurate scans without image distortion. Stackable and Space-Efficient: Every square foot counts in an airport. Mexeltec tubs stack neatly, maximizing storage space and reducing clutter at checkpoints. Optional Features for Safety and Hygiene: Anti-slip bases prevent items from shifting, while antimicrobial materials improve hygiene in high-touch areas — a must in post-pandemic travel. These details may seem small, but when you multiply them by thousands of trays across hundreds of daily flights, the efficiency gains are enormous. 3. Meet the Mexeltec Lineup: Engineered for Every Need Mexeltec doesn’t believe in one-size-fits-all. Their product range caters to every operational need, from passenger screening to baggage conveyor systems. Here’s a quick overview: CRS 600 Security Tub Ideal for security checkpoints and X-ray scanning areas. Durable, ergonomic, and designed to glide effortlessly through conveyor belts. CRS 900 & CRS 990 Baggage Handling Tubs Built for Baggage Handling Systems (BHS). Their reinforced structure handles heavy loads, from suitcases to odd-sized luggage, without deformation. Each model is designed for long service life — meaning less frequent replacements and lower total cost of ownership. That’s the kind of value airports love. 4. The ROI of Smarter Baggage Tubs Let’s talk numbers — because every operations manager cares about ROI. Imagine two airports: Airport A uses standard, low-cost tubs that crack every few months. Airport B uses Mexeltec’s high-durability tubs that last 5x longer. Airport A might save upfront, but over time, the replacements, inefficiencies, and downtime costs far more. Mexeltec tubs reduce long-term costs in three ways: Fewer Replacements: Their HDPE construction withstands constant use. Faster Throughput: Ergonomic design speeds up handling. Lower Maintenance: Smooth surfaces mean fewer snags and jams in the system. In other words, Mexeltec tubs don’t just move luggage — they move profits. 5. Global Standards, Local Expertise Mexeltec isn’t new to this game. As a trusted airport equipment manufacturer in India, they serve airports and logistics hubs across the country — and their reputation is growing globally. Their products meet international aviation standards and are tested for real-world durability and X-ray performance. When you buy Mexeltec, you’re not just buying tubs; you’re partnering with a company that understands aviation operations, material science, and airport logistics inside and out. 6. Sustainability That Scales Modern airports are under pressure to go green. Mexeltec contributes to sustainability by manufacturing long-lasting tubs that reduce plastic waste and cut down on energy-intensive replacements. Durability = fewer replacements = less landfill waste. Plus, HDPE is recyclable, aligning with global environmental initiatives for a more circular economy. 7. Why Airports Choose Mexeltec Still wondering why more airports are switching to Mexeltec’s tubs? Here’s what decision-makers cite most often:  ✅ Long-term durability and impact resistance ✅ Seamless integration with X-ray and conveyor systems ✅ Customization for different airport zones ✅ Hygienic, anti-slip, and space-saving designs ✅ Competitive pricing and dependable local support When efficiency, hygiene, and longevity matter, Mexeltec is the name airports trust. 8. Ready to Upgrade Your Airport Operations? Think of it this way — every time a bag, laptop, or jacket passes through security, it’s an opportunity for efficiency or delay. The right baggage tubs turn that moment into a win. So, if you’re ready to: Speed up screening, Reduce equipment wear, and Create a better passenger experience… Then it’s time to invest in Mexeltec’s Baggage Tubs. ???? Visit the Mexeltec Baggage Tubs Page to explore the full range and request a quote today. Final Thoughts Efficiency isn’t just about cutting-edge tech or expensive automation. Sometimes, it’s about getting the basics right — and baggage tubs are one of those fundamentals. Mexeltec has taken something simple and turned it into a powerful tool for operational excellence. “Don’t chase the next big trend before you optimize what’s right in front of you.” So start small, think smart, and choose the tubs that make a big impact.  

How the Right Baggage Tubs Can Transform Airport Efficiency (and Why Mexeltec Leads the Way) Read Post »

This will close in 20 seconds

Scroll to Top